How to calculate sewing line efficiency
@rgemas · · 8 min read
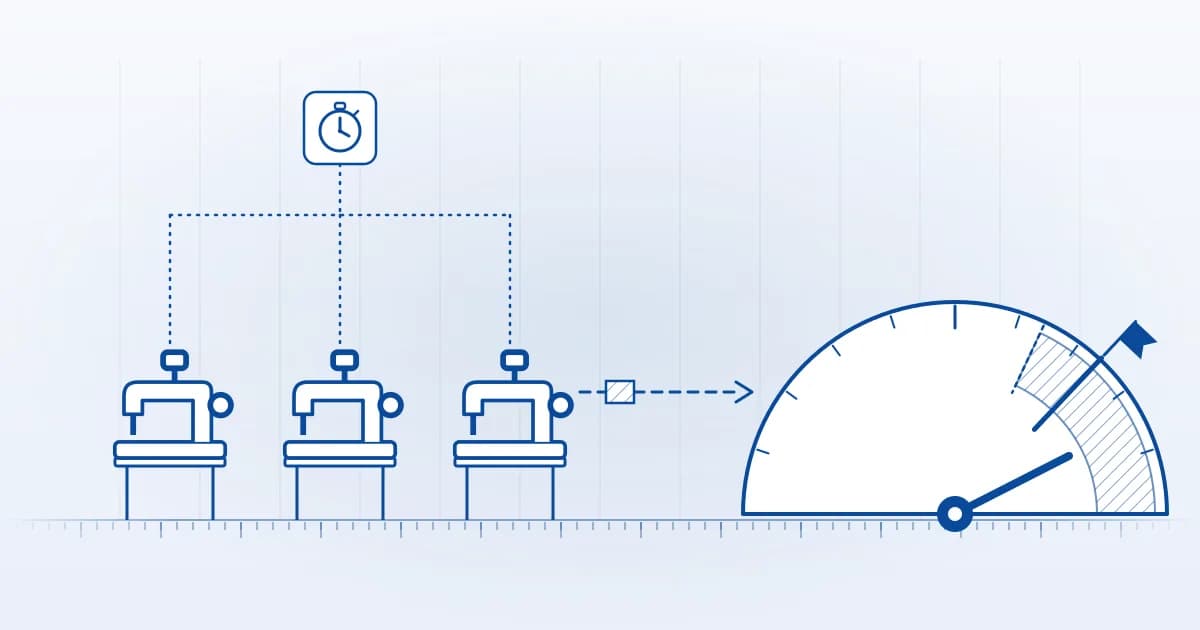
A garment plant manager usually has three numbers to hand: the pieces the line produced by the end of the day, the number of operators on it and the length of the shift. The efficiency question follows from them: “Is this line running well?” This post shows how to answer with a number: the formula, the missing fourth input (standard time), how lost time enters the calculation and the efficiency at which the line starts to earn money.
For the method we use the definition on our sewing line efficiency measurement page. The worked numbers come from the 2022 paper by Assoc. Prof. Aydın Koçak and Hulisi Ayluçtarhan, “Konfeksiyon İşletmelerinde Verimlilik ve Kalite Temelli Bilgisayar Destekli Bir Prim Sistem Modeli” (in our translation, “A Computer-Aided Bonus System Model Based on Productivity and Quality for Garment Businesses”), published in the Üçüncü Sektör Sosyal Ekonomi Dergisi. The paper is in Turkish; the title and all quotations are our translation. Its lira figures date from 2022; the ratios are what matters. Examples and readings that are not in the paper are marked “our example” or “in our view”.
The formula: minutes produced over minutes worked
Sewing line efficiency is the share of labour time that turns into production. For every operator and every operation, the pieces produced are multiplied by that operation's standard time and divided by the time the operator actually worked:
The numerator is the “minutes produced”: the operator's output expressed in standard minutes. The denominator is the real minutes spent producing it. Both are in the same unit, so the result is a percentage, and different operations, products and lines can be compared on it.
The paper's example comes from a line where pieces travel on trolleys:
A standard scenario: trolley capacity 20 pieces, standard time of the operation 0.5 min; if the operator produces 50 trolleys over the day, efficiency is calculated as
Step by step: 50 trolleys × 20 pieces = 1,000 pieces. 1,000 pieces × 0.5 minutes = 500 minutes produced. The shift is 540 minutes (08:00 to 18:00 with an hour for lunch). .
The only outside input is the standard time: how many minutes an operation should take a qualified operator working at normal pace. Standard times come from predetermined time systems such as MTM or from a stopwatch; the methods are on our MTM and standard time measurement page. If the standard time is missing or out of date, the rest of the formula can be right and the result still wrong.
Operator efficiency and line efficiency are the same formula at two scales
The example above measures one operator. For the whole line, the numerator is the sum of the minutes produced across all operations and the denominator is the sum of the minutes all operators worked.
Our example, with hypothetical numbers: a line of 30 operators on a 540-minute shift. The standard times of all operations on the garment add up to 12 minutes. 1,000 pieces came off the line by the end of the day.
- Minutes produced: minutes
- Minutes worked: minutes
This shortcut assumes the work in progress inside the line is about the same at the start and the end of the day; if the line is filling or draining, the output count does not show the day's work in full. Measuring per operator solves this on its own, because every operation's pieces are counted separately.
Lost time: taken out of the denominator, never out of sight
Not every minute of the shift goes into sewing. Machine breakdowns, waiting for material and thread changes are factory-caused stoppages outside the operator's control. Our sewing line page draws the distinction this way: lost time is measured separately from efficiency, so you can see how much of a 540-minute shift went into production and how much into which loss, and the operator's efficiency is calculated net of those losses.
Continuing our example. Same operator, same 500 minutes produced, but 60 minutes of the day spent waiting for material.
Both numbers are needed. The first measures the operator's performance and bonus: the waiting minutes were not their fault. The second is the line's and the factory's efficiency: those 60 minutes were paid for and produced nothing. In our view the common mistake is choosing one of the two; the first alone hides the losses, the second alone penalises the operator unfairly.
Quality is a separate factor
The paper does not fold quality into efficiency; it calculates it separately, as a coefficient on the efficiency-based bonus:
If the operator produces 1300 good pieces and 250 rejects during the day, the quality rate is
Efficiency answers “how much work came out”, quality answers “how much of it was good”. Merging the two into one number hides which one has dropped.
At what efficiency do you make money?
An efficiency percentage is neither “good” nor “bad” on its own; the cost side gives it meaning. The paper builds this on two per-minute figures. The first is what one minute of one operator costs the business:
Based on monthly expenses (energy, wages, meals, social security, building and machine maintenance, etc.), the cost per minute per operator is calculated with the formula
The second is what one standard minute earns the business: the total labour price of the products made in the month, divided by the total standard minutes of the same products. The paper's application scenario (Table 1) gives the two figures as follows:
- Monthly cost per operator 8,000 TL, 20 days a month, 540 minutes a day: cost per minute 0.74 TL
- From the customer labour prices of a shirt, dress A and dress B mix: revenue per minute 1.15 TL
- Break-even point:
- Bonus limit with a 15% target profit: , about 400 minutes a day
Read it this way: on this line an operator covers their cost once 64% of the shift turns into minutes produced. Above 74% the business has earned its target profit, and in the paper's model everything above that is shared with the workers. The paper tabulates the same logic for a 55-person line (Table 3); in that scenario workers earn no bonus when efficiency falls below 74%, and below 50% the line starts to lose money. The authors note one more use of that table: a manager can run the break-even analysis for customer quotations with it.
The numbers belong to 2022 and to that line. Your cost and revenue per minute will both differ; what does not change is that their ratio gives the efficiency threshold.
Do your own calculation
Our worksheet. Collect the following for one shift; apart from the standard time, most factories already have them.
- Pieces off the line at the end of the day (A)
- Sum of the standard times of all the garment's operations, in minutes (B)
- Number of operators on the line (C)
- Shift length, in minutes (D)
- The line's total lost time that day, in minutes (E)
Three more numbers for the profit threshold:
- Total monthly cost per operator (F)
- Working days in the month (G)
- The month's labour revenue ÷ the month's total standard minutes produced (H)
If you do not have B, that is a finding in itself: the line's efficiency has so far been estimated, never measured.
Four habits that break the calculation
In our view these are the most common mistakes on the shop floor:
- Stale standard times. The method, machine or style has changed and the time has stayed the same. The efficiency percentage rises or falls while the line runs exactly as before.
- Putting attendance hours in the denominator. The clock-in to clock-out time in the attendance system and the time spent at the machine are two different things; the gap between them should show up separately as lost time.
- Comparing lines by piece count. A line that makes 1,000 shirts and one that makes 600 jackets can only be compared on minutes produced.
- Counting rejects as production. If a defective piece also earns minutes, efficiency covers up quality. Track quality as a separate factor, as the paper does.
A daily spreadsheet or real-time measurement?
This calculation can and should be done every day in a spreadsheet; the result is yesterday's number. To see the line as it is right now, pieces have to be counted per operator and per operation as they are produced. In the method described on our sewing line page, every bundle is tracked from operator to operator with a barcode or RFID tag; lost time is started and stopped by scanning a card on the IoT device, and the time between the two is recorded automatically as lost time. The measured efficiency and quality scores also flow in real time into the bonus and fair pay system.
The paper's conclusion describes what real-time measurement does on the management side:
When a worker earns no bonus because they worked inefficiently, they give feedback to their manager, which creates the opportunity to identify and resolve bottlenecks in the process quickly.
If you would like to work out your line's efficiency and profit threshold with us, the factory analysis starts with this calculation. How to test the method in a vendor demo is in our post on what to ask in an MES demo.
Sources
- Koçak, A. & Ayluçtarhan, H. (2022). Konfeksiyon İşletmelerinde Verimlilik ve Kalite Temelli Bilgisayar Destekli Bir Prim Sistem Modeli [A Computer-Aided Bonus System Model Based on Productivity and Quality for Garment Businesses]. Üçüncü Sektör Sosyal Ekonomi Dergisi, 57(3), 1805–1823. Full text (Turkish); a summary is on our academy articles page.
- argemas: Sewing line efficiency measurement and MTM and standard time measurement.
Share this post